Case Overview
A dairy and beverage processing-line manufacturer encountered cleaning-validation failures on new pasteurization and CIP skids: product-contact surfaces rougher than specified retained bacteria after cleaning, while heating elements produced inconsistent output across the line. Both problems traced to material supply: the previous supplier had not controlled internal tube roughness or heating-wire resistance.
DZX qualified with hygienic 316L tubes at internal Ra ≤ 0.4 μm and heating-element wire at ±5% resistance per meter, closing cleaning-validation and heating-uniformity gaps through one supply chain.
This case summarizes the application requirements, materials supplied by DZX and delivery value. For case-specific technical data, please contact our engineering team.
| Item | Details |
|---|---|
| Client Profile | Dairy and beverage processing-line manufacturer |
| Project Scale | Multiple pasteurization and CIP skids built annually |
| Application | Product-contact piping, process heating and temperature control |
| Materials Supplied | 316L stainless steel tube, NiCr/FeCrAl heating-element wire and thermocouple alloys |
| Supply Forms | Tube, wire and strip |
| Lead Time | Standard sizes: 2-3 weeks; custom: 4 weeks |
| Project Country | Denmark |
| Project Year | 2025 |
Our Solution
The manufacturer’s quality system exposed three material-related problems:
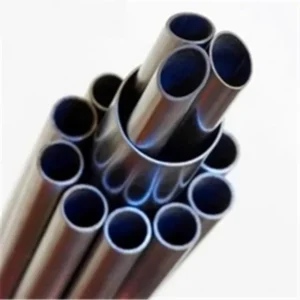
- Cleaning-validation failure: product-contact tubes with internal roughness above Ra 0.4 μm retained soil after CIP, repeatedly delaying line commissioning.
- Uneven process heating: elements assembled from uncontrolled wire produced output outside their rated range, causing pasteurization temperature drift.
- Poor sensor consistency: monitoring probes made from thermocouple wire with overly loose EMF tolerances delayed calibration acceptance.

DZX organized supply around the manufacturer’s validation requirements:
Hygienic 316L tubes were verified at internal Ra ≤ 0.4 μm, with documentation for the cleaning-validation file. NiCr and FeCrAl element wire was drawn with resistance per meter controlled within ±5% for consistent heating. Thermocouple alloy wire included IEC 60584-1 EMF verification for temperature control. Every batch included roughness, resistance and calibration documentation.
| Material | Representative Grades | Key Properties | Available Forms |
|---|---|---|---|
| Stainless steel | 304、316L | Hygienic surface and corrosion resistance | Tube and strip |
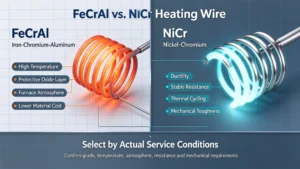
| NiCr / FeCrAl | Cr20Ni80、0Cr21Al6 | Process heating elements | Wire and strip |
| Thermocouple alloys | K、T | Temperature control | Wire and cable |
View Stainless Steel Alloys → | View NiCr Alloys → | View Thermocouple Alloys →

CIP and product piping

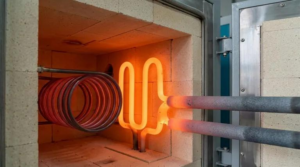
Cr20Ni80 heating elements

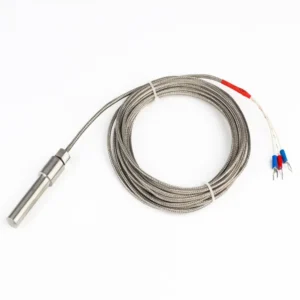
Pasteurization and sterilization temperature measurement
Technical Specifications
Key technical parameters agreed before production. Contact us for grade-specific datasheets and tolerance-verification reports.
| Parameter | Agreed Specification | Verification Method |
|---|---|---|
| Tube internal surface roughness | Ra ≤ 0.4 μm (product contact) | Batch profilometer testing |
| Tube dimensions (typical) | 38 mm OD × 1.5 mm wall | Micrometer + thickness measurement |
| Heating-element wire resistance | ±5% of nominal Ω/m | Coil-by-coil resistance testing |
| Thermocouple EMF | IEC 60584-1 | Batch calibration reports |
| Surface cleanliness | Passivated and oil-free | Cleanliness + visual inspection |
Each supplied batch includes a quality inspection certificate with chemical analysis, meeting the applicable standard for each grade.
| Material | Applicable Standards |
|---|---|
| Stainless steel | ASTM A270 (hygienic tubing), A240 |
| Heating-element wire | GB/T 1234、ASTM B344 |
| Thermocouple alloys | IEC 60584-1 |
| Quality System | Inspection certificate including chemistry and roughness reports |
Delivery and Quality Support
- Fast delivery: Sample and production lead times follow the project schedule; standard grades and sizes can be dispatched promptly from stock.
- Quality traceability: Every batch includes material certificates and inspection reports, with full heat and batch traceability.
- Technical support: Responsive support covers pre-sale material selection, drawing review and post-sale processing advice.
- Ongoing service: Regular follow-up after delivery tracks performance and addresses feedback promptly.
Customer Feedback
- Cleaning validation passed: measured internal Ra ≤ 0.4 μm closed the CIP validation gap
- Consistent heating: ±5% heating-wire resistance eliminated pasteurization temperature drift
- Faster line acceptance: calibration-ready thermocouple wire shortened commissioning
- Auditable records: batch roughness, resistance and calibration reports
- One supplier, three needs: tubes, heating elements and sensors coordinated under one quality system
- Reliable delivery: standard sizes in 2-3 weeks, aligned with line-build schedules
Our Capabilities
Jiangsu DZX Technology Co., Ltd. (Changzhou DLX Alloy) was founded in 2016. Its core team has worked in the field since 2002, with 24 years of precision-alloy R&D and production experience, operating a self-owned 12,000-square-meter modern factory with an ISO9001 system covering three inspection stages. Annual alloy output exceeds 1,200 tonnes, serving 1500+ business customers worldwide. The company operates integrated melting, drawing, annealing and precision-machining workshops, supporting volume customization of strip, wire, tube and bar. Every batch includes a chemical analysis report (MTC) for full delivery-quality traceability.
Related Products
Food Applications
Food processing, brewing and dairy, temperature control and hygienic systems
Residential Applications
Heating elements, cookware, HVAC controls and electrical protection
Industrial Applications
Furnace heating, heat treatment, machinery and wear-resistant parts